China Beverage Production Line Manufacturer: How to Choose the Right Partner for Your Facility
2026-09-10
You've probably heard that China is the place to buy beverage production lines—lower costs, fast delivery, endless options. But here's what most facility managers don't realize until it's too late: the real difference isn't in the machine spec sheet, it's in the partner behind it. A single wrong choice in supplier can stall your entire operation for months. That's why we're sharing what we've learned on the ground at INTOP Machinery—not as a sales pitch, but as a practical filter for separating the truly reliable Chinese manufacturers from the ones that just look good on paper.
Assess Their Experience with Your Specific Beverage Type
Most people won't tell you straight away what they think of a particular drink. If you want an honest read, stop asking yes-or-no questions and invite them to describe the texture, the way sweetness hits, or how long the aftertaste lingers. Someone who has experience with your beverage type will mention details you didn't prompt for, while a newcomer will lean on vague words like 'smooth' or 'refreshing.' That distinction matters more than a five-star score.
Better still, hand them a small sample and just watch. A seasoned drinker of that category might swirl, sniff, or take a tiny first sip before committing. A less familiar taster will often gulp, wince, or set the cup down and forget it. Afterward, ask what they would change—not what they liked. Their answer usually exposes how deeply they actually know the drink you're making.
Look Closely at Their In-House Manufacturing Capabilities
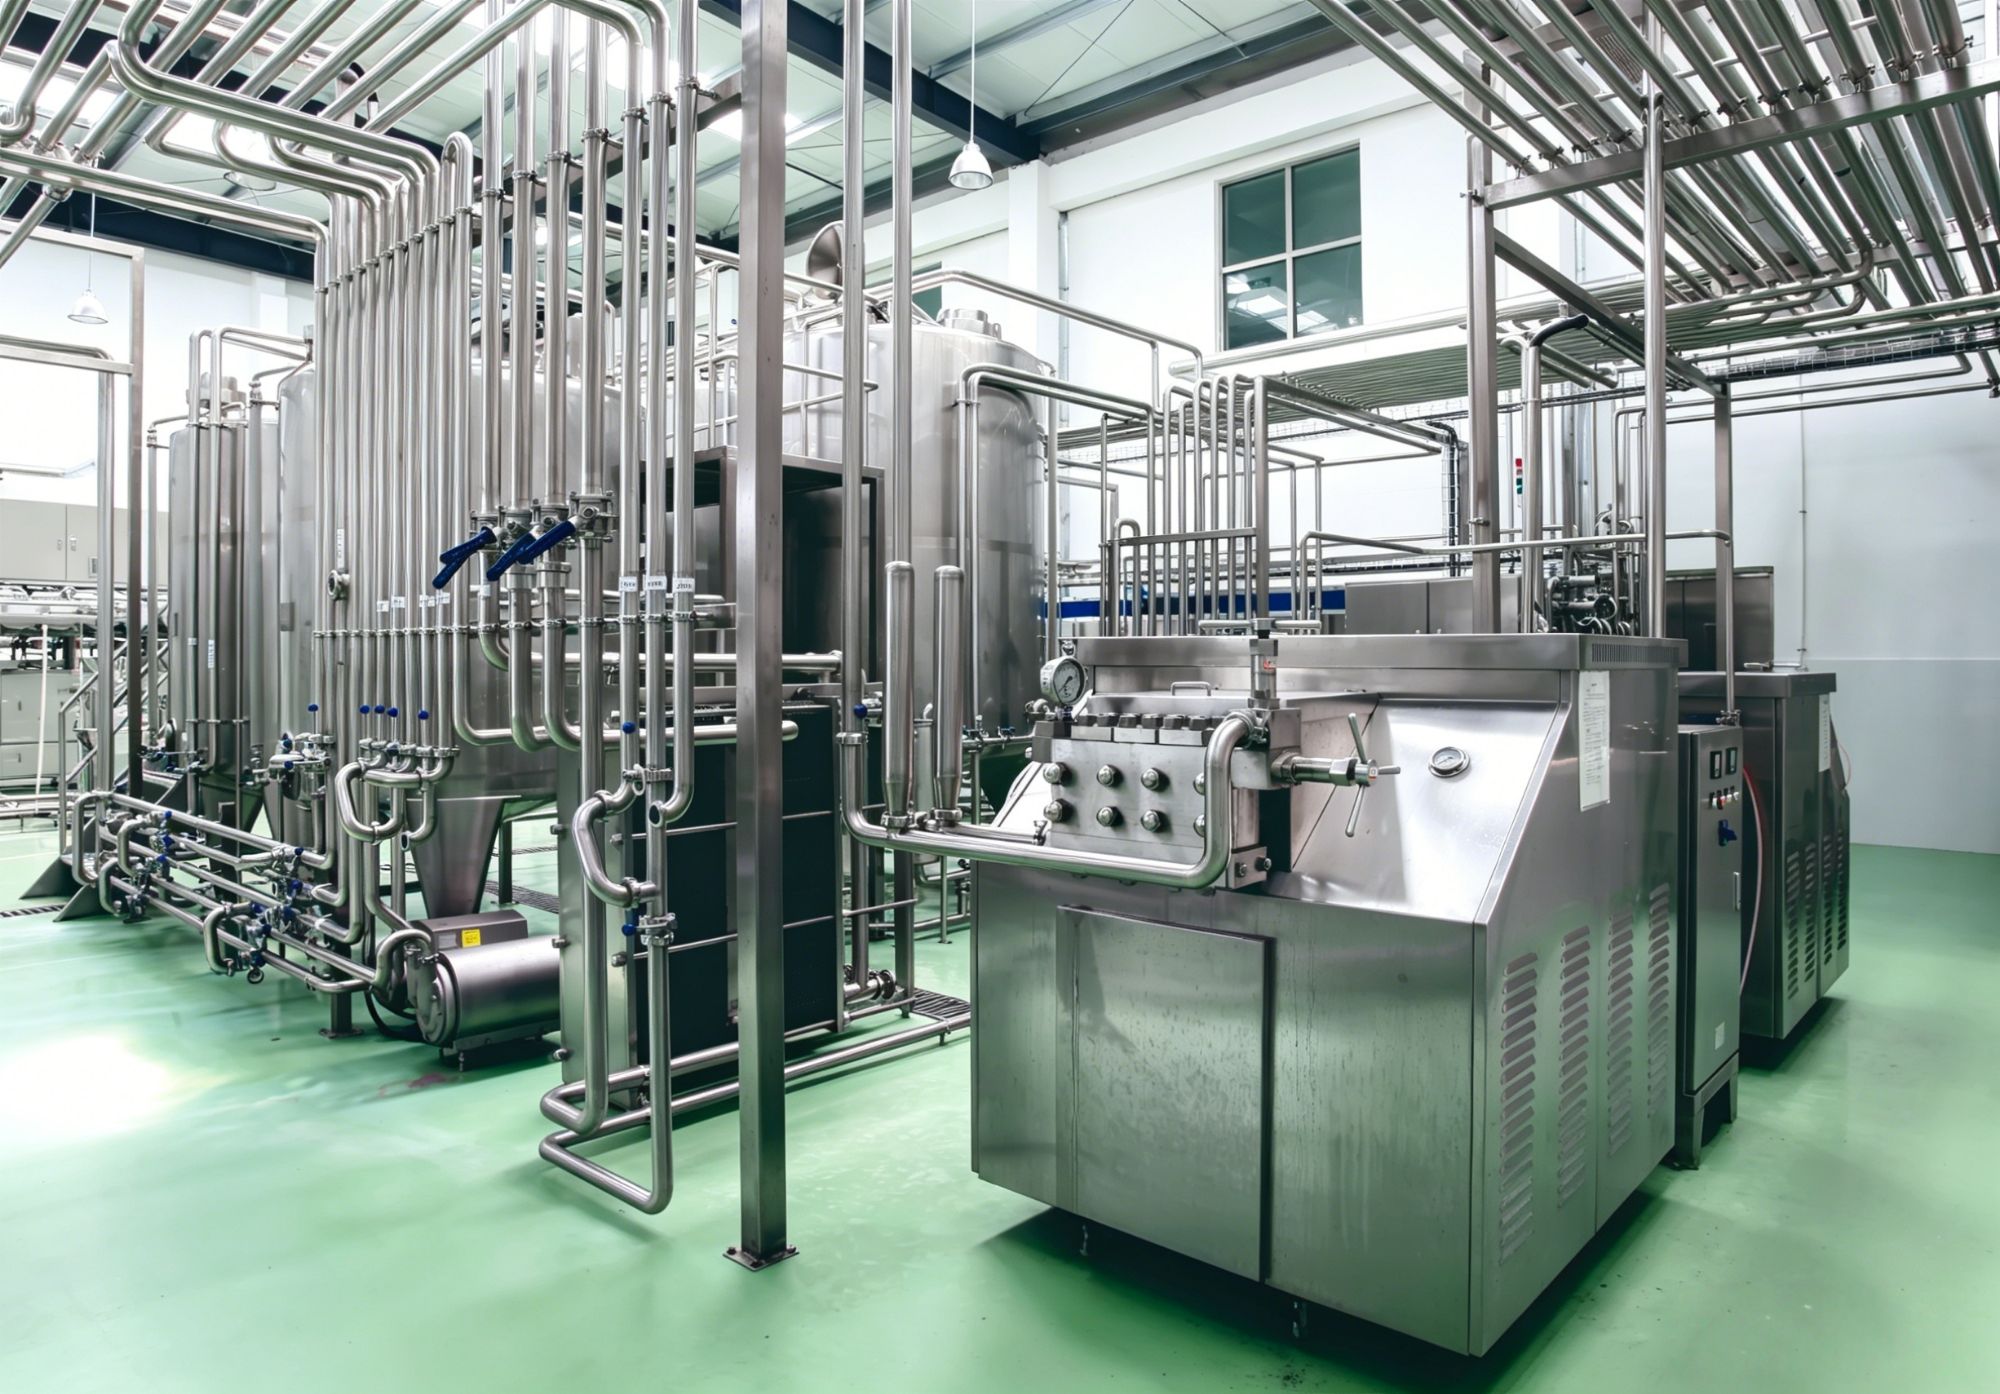
A supplier’s claims about quality mean little if they don’t actually do the work themselves. When you look closely at in-house manufacturing capabilities, you’re checking whether they control the production process or just coordinate other shops. This matters because every handoff to an outside vendor adds delay, miscommunication, and potential quality drift. A company that runs its own CNC machines, injection molding, or assembly lines can usually spot problems earlier and fix them without waiting on a third party. Ask to see the floor, not a presentation.
Beyond the basic equipment list, pay attention to how the facility is organized and whether the staff seem familiar with the machines. Real in-house capability shows up in small details: custom jigs lying around, a tool room that’s actively used, or technicians who can explain why a certain material behaves differently under stress. If a supplier hesitates to let you visit, or only shows you a polished conference room, that’s a red flag. You want to see raw material coming in one door and finished parts going out another, ideally with quality checks at each critical step.
Also ask about their capacity for your specific project. Having a machine is not the same as having the right tooling, programming expertise, or spare capacity. A shop might own a 5-axis mill but rarely use it for complex geometries, so your job becomes their learning curve. Probe with real scenarios: how would they handle a tolerance issue discovered mid-run? What’s their typical scrap rate? Do they perform in-process inspection? Their comfort level with these questions reveals whether in-house manufacturing is a genuine strength or just a brochure bullet point.
Ask How They Handle Line Design and Layout Planning
You can learn a lot about a factory's real capabilities by digging into how they approach line design and layout planning. Instead of accepting vague assurances, ask for a walkthrough of a recent line they built: why equipment was placed in that order, what material flow looked like, and where they left room for changeovers or future expansion. Their answer—or lack of one—often reveals whether they treat layout as a one-time sketch or as a living part of production.
A strong partner will talk about balancing operator movement, minimizing travel distance for parts, and keeping quality checks close to the point of assembly. They should be able to point to specific constraints they faced, such as ceiling height, column spacing, or power drops, and explain how the layout worked around them. Listen for details that only come from hands-on experience, like how they staged incoming materials to avoid double handling or how they kept a new line from disrupting existing ones during installation.
It is also worth asking how they validate a layout before committing to it. Some teams use cardboard mock-ups or 3D simulations; others run a pilot cell first. What matters is that they can describe a repeatable process for spotting bottlenecks and adjusting before full production starts. If their answers stay at the level of "we follow lean principles," push for a concrete example—the more specific the story, the more likely that their planning approach will hold up when your product hits the floor.
Verify Their Quality Control and Compliance Record
A supplier's certifications tell only part of the story. What matters more is how those standards hold up under real production pressure. Ask for detailed batch inspection reports, not just final product sign-offs. Look at the frequency of their in-process checks, the calibration records for testing equipment, and whether they maintain a live non-conformance log. Any hesitation in sharing these documents usually indicates trouble below the surface.
Dig into their compliance history with specific regulatory bodies relevant to your industry. Are they registered with the FDA, EPA, or EU REACH? Have they faced any import holds or warning letters in the past three years? Cross-check their claims against public databases where possible. A supplier who proactively volunteers audit schedules and corrective action plans demonstrates a culture of transparency that paper certificates alone cannot prove.
Finally, verify through third-party sources. Contact their previous clients in a similar product category and ask about defect rates, on-time corrective responses, and whether the supplier ever shipped product that failed independent lab testing. Visit their facility unannounced if feasible, or commission a surprise audit. Quality control is a daily practice, not an annual event, and the way a supplier handles discrepancies reveals far more than any polished compliance brochure.
Understand Their After-Sales Support and Spare Parts Network
A supplier’s after-sales support often reveals more about their reliability than any sales pitch. Look beyond the initial warranty period and ask how quickly they respond when a machine goes down. Field service availability, remote diagnostics, and a clear escalation path matter more than a glossy service brochure. Some manufacturers promise round-the-clock assistance but rely on third-party contractors who may not know the equipment well. Others keep a dedicated team that can walk your technicians through repairs over the phone before dispatching anyone.
Spare parts are where downtime gets expensive. A machine that’s out of service for two weeks because a single bearing had to be shipped from overseas can wipe out the savings from a lower purchase price. Check whether critical components are stocked locally, how orders are prioritized for production-stopping failures, and whether the supplier offers refurbished or alternative parts for older models. The best networks combine regional hubs with a streamlined ordering portal that shows real-time inventory instead of forcing you to email a sales rep and wait.
The real test comes when a part is discontinued. Some companies leave you scrambling to find aftermarket replacements or cannibalize your own machines, while others maintain backward-compatible inventories or provide detailed CAD files so a local machine shop can recreate simple components. Before signing a purchase order, ask for examples of how they handled unscheduled downtime for existing customers in your region. If they hesitate to share references or their support team is hard to reach during the sales process, that pattern will likely continue after the invoice is paid.
Compare Total Cost of Ownership, Not Just Initial Quotes
A vendor's opening price looks decisive only if you ignore what happens after installation. Power draw, consumables, spare part lead times, and the labor needed for routine upkeep all compound over the asset's life. In many plants, a unit with a 9% higher sticker price ends up cheaper within eighteen months because it consumes less electricity and holds calibration longer. Procurement that stops at the quote misses this entirely.
Build a basic TCO model before requesting bids. Ask each supplier to submit energy consumption at your expected load, recommended service intervals, and typical part replacement costs over five years. Then run the numbers yourself rather than trusting their summary. You'll often find that two machines with nearly identical specs diverge sharply once operational expenses enter the spreadsheet. The more boring the line item—seals, filters, software licenses—the more likely it is to flip the decision.
Ignore the temptation to treat TCO as a tiebreaker only when quotes are close. A truly lower ownership cost can justify a much higher initial outlay, especially when downtime is expensive. The goal isn't to buy the cheapest asset; it's to buy the one that costs least to own across its useful life.
FAQ
Look beyond equipment catalogs. A dependable partner will ask about your product viscosity, carbonation level, fill temperature, and bottle shape before quoting anything. They should challenge your assumptions—for instance, pointing out if a hot-fill line would suit your tea drinks better than your initial aseptic idea. If a manufacturer only talks price and delivery date without understanding your liquid, move on.
Request video walkthroughs of their current assembly floor and recent installations, not just polished brochures. Ask them to show a live test on a line similar to yours, with bottle jams or cap misfeeds triggered intentionally. You can also ask for references in your beverage category and speak to plant managers who have run those lines for at least a year. Third-party inspection reports from agencies like SGS or TÜV add another layer, but real user feedback carries more weight.
Many quotes exclude installation supervision, operator training, and even essential wear parts like filling valves or conveyor belts. Ask for a line-item breakdown that includes commissioning time, travel expenses for their engineers, and spare parts recommended for the first two years. Also check whether the quoted speed is based on nominal output or actual sustained output with changeovers—some manufacturers inflate capacity by assuming perfect conditions.
Send physical samples, not just CAD drawings. Bottle neck finish, cap torque, and label material all affect line design. Request a trial run on their own test conveyor using your bottles and caps, and have them record the reject rate at your target speed. If they cannot accommodate a trial, that is a red flag. A good manufacturer will often modify grippers, star wheels, and fill nozzles based on trial data.
Get specific response times in writing: how fast do they respond to a breakdown call, and do they offer remote diagnostics? Ask whether spare parts are stocked in your country or only shipped from China, and what the typical lead time is for critical parts like PLC modules or servo drives. Also clarify if their engineers can support your local maintenance team via video call, or if an on-site visit is mandatory for every issue.
It depends on your risk tolerance and project complexity. Large groups might offer a one-stop solution with more polished project management, but your line may get less individual attention. Smaller specialized builders often have deeper experience with a particular beverage type—like dairy, juice, or carbonated drinks—and can be more flexible with customizations. Check their track record for your exact product category, not just their overall sales volume.
Talk to operators, not just owners. Ask recent clients how many unplanned stops they had in the first six months, what the mean time between failures was for filling heads, and how often they had to recalibrate the capping machine. Request maintenance logs if possible. Also look at the design of critical components: are bearings sealed and food-grade? Are sensors from reputable brands? Simple, accessible designs usually outlast complex proprietary systems.
Include acceptance testing at their factory before shipment, and again after installation at your site with agreed performance metrics like output rate, fill accuracy, and reject rate. Stipulate that payment milestones are tied to these tests, not just delivery. Also require a warranty period covering parts and labor for at least 12 months after commissioning, and specify penalty clauses for delayed installation or missed performance targets. Avoid contracts that allow them to substitute components without approval.
Conclusion
Picking a production line partner in China isn't about who sends the longest equipment list. Start by digging into their track record with your exact product, whether that's carbonated soft drinks, dairy, juice with pulp, or ready-to-drink tea. A line that handles still water beautifully can struggle with viscosity, carbonation levels, or hot-fill requirements. Look for a manufacturer that asks about your recipes, bottle shapes, cap types, and target output before quoting anything. Then examine what they actually build under their own roof. Companies with real in-house machining, welding, and assembly tend to control tolerances better and respond faster when something needs adjusting. Ask to see photos or video of their current workshop floor, not just a polished brochure. Equally important is how they approach line design. The best suppliers don't just stack machines; they study your facility's ceiling height, power supply, drainage, and personnel flow. They should propose a layout that trims transfer points and reduces changeover time, rather than squeezing in as many units as possible.
Quality control and compliance are non-negotiable, so request documentation on material certifications, pressure vessel standards, and any export history to your region. A manufacturer that openly shares test reports and invites third-party inspection is far less risky than one that dodges specifics. Then, look past the sale. Ask hard questions about after-sales support: do they have remote troubleshooting in your time zone, how quickly can they ship wear parts, and will they send an engineer for commissioning? A machine that sits idle for three weeks waiting on a small sensor costs more than any upfront discount. Finally, compare total cost of ownership. Factor in energy consumption, spare parts pricing, local service availability, and expected lifespan of key components like fillers and cappers. A slightly higher quote from a supplier with a nearby parts hub and documented uptime records often beats a cheaper line that quietly drains your maintenance budget. Choose the partner who treats your facility's constraints as the starting point, not an afterthought.
Contact Us
Contact Person: Laura
Email: [email protected]
Tel/WhatsApp: +86 13957758832
Website: https://www.intopmachinery.com