Custom Tact Switch Supplier: What to Look for Before Partnering
2026-10-16
Choosing a custom tact switch supplier is more than a procurement task—it’s a design decision that can make or break your product’s feel, durability, and user experience. Before you sign a partnership, you need to look past spec sheets and sample kits. From actuation force consistency to lead time transparency, the details matter. At KEJIAN ELECTRONICS, we’ve seen too many design teams burn time fixing issues that could have been avoided with a smarter supplier evaluation. Here’s what actually deserves your attention before you commit.
Engineering Depth Beyond Standard Catalogs
Most catalogs stop where real applications begin. Standard components solve standard problems, but the moment a load path shifts, a thermal gradient appears, or an envelope shrinks, off-the-shelf answers get quiet. Our engineering starts there—not by hunting for a part number, but by mapping the actual forces, tolerances, and failure modes behind your requirement.
That depth shows up in the details: custom bearing preloads calculated from measured runout, gear tooth profiles adjusted for low-speed high-torque wear, materials selected for chemical exposure that never appears in a datasheet. We prototype, test to destruction, and revise until the component behaves like it was always meant to be there.
The result is not a special item with a longer lead time and a premium price tag. It is a set of design choices made deliberately—so your assembly fits, holds, and lasts without forcing your project into someone else's product boundary.
Material Traceability and Honest Trade-offs
Tracing a material back to its source sounds tidy on a spreadsheet, but the physical world rarely cooperates. A single shipment of cotton, cobalt, or recycled polymer may pass through five or six sets of hands, each with its own paperwork, storage conditions, and mixing points. Some records are handwritten, some are digital, and a few simply disappear when a broker changes suppliers mid-order. The result is that even well-intentioned companies often know less about their supply chains than their marketing language suggests.
The honest trade-off is that full traceability costs real money and time, and it can quietly push smaller producers out of the picture. A family-run tannery in Portugal might not have the blockchain-ready documentation system that a large conglomerate can afford, even if its environmental record is better. Some manufacturers now admit that certain recycled-content numbers are based on mass balance rather than physical tracking, meaning the specific molecules in a given product may not be the ones that came from a recovered bottle. That is not fraud; it is a declared limitation.
What separates a credible claim from a decorative one is whether the company names the gap. Instead of saying “fully traceable,” a more useful statement might be “we can trace origin to the spinning mill, but not to the farm gate” or “our recycled fiber percentage is certified through a mass-balance system.” That level of candor is rare, yet it gives designers, buyers, and regulators something concrete to evaluate. Pretending the chain is unbroken does not make it so, but acknowledging where the thread gets thin does make the rest of the story easier to believe.
From First Sample to Mass Production: Where Things Break
The jump from a working prototype to a production line rarely fails in the ways people expect. The first sample often hides its flaws because it was built by hand, with carefully selected components and plenty of quiet troubleshooting. On the factory floor, however, the same design must survive the chaos of real tolerances, mixed batches, and operators who have never seen the original bench notes. That is where the first cracks appear: a connector that fits perfectly in the lab but jams after a thousand insertions, or a plastic clip that holds fine in a single unit but warps when molded in a 16-cavity tool.
Scale also changes the nature of failure. A single sample can be reworked, polished, or tuned until it behaves. Mass production removes that safety net. Suppliers substitute materials to hit a price target, assembly jigs drift from their CAD models, and inspection criteria quietly loosen under schedule pressure. The problems stop being about whether the design works and start being about whether the process can repeat it ten thousand times without someone making an undocumented adjustment. Often the breaking point is not a dramatic part failure, but a slow accumulation of small deviations that only becomes visible when units ship with intermittent defects.
The most dangerous shift is cultural. Engineers treat the first sample as a proof of concept; factories treat it as a promise of yield. When the conversation moves from the workbench to the production meeting, the assumptions change. What was once a known quirk becomes a hidden cost. Without a deliberate handoff—where tolerances, critical dimensions, and assembly sequences are challenged under realistic conditions—the gap between sample and production grows quietly until it becomes a recall, a warranty claim, or a line shutdown.
Quality Checks That Go Beyond a Final Inspection
A final inspection often serves as a safety net, but it cannot catch every flaw that has already been woven into a product. By the time a defect is found at the end of the line, the cost of rework or scrap has already compounded. Instead of relying on that last gate, forward-thinking teams shift their focus to earlier, more granular checkpoints—where small adjustments cost pennies rather than dollars.
In practice, this means embedding quality checks directly into each stage of production. Operators perform quick in-process measurements, sensors track critical parameters in real time, and suppliers are held to agreed tolerances before materials ever reach the floor. These touchpoints act as ongoing conversations with the process, surfacing drift or wear long before it becomes a nonconformance.
Ultimately, quality beyond the final inspection is less about adding more checks and more about building a culture where everyone owns the outcome. When a machinist pauses to verify a setup, or a packer flags a mislabeled box, the product is being protected while it is still being made. That collective vigilance turns quality from a gate at the end into a habit throughout the journey.
When Your Supplier's Supplier Becomes Your Problem
Most companies keep a close eye on their direct vendors, but few track the suppliers behind those vendors. A missing bolt from a third-tier machine shop can idle an assembly line just as quickly as a primary supplier's missed shipment. The chain is only as strong as its least visible link.
When a sub-tier supplier files for bankruptcy, loses a key customer, or hits a raw material shortage, the shock travels upward. Purchase orders get pushed back, quality slips, and delivery promises to your own clients start to look like guesswork. By the time you notice, the problem has already become yours.
The fix isn't more paperwork. It's asking direct suppliers for their critical supplier lists, mapping shared dependencies, and building buffer stock for the few components that can't be sourced elsewhere quickly. Visibility into the second tier turns a surprise failure into a manageable risk.
Communication Habits That Predict Project Success
Successful projects rarely hinge on what gets said in formal status meetings. Instead, they rise or fall on the small, repeated ways team members talk to each other between meetings. One of the strongest predictors is how often people ask direct questions rather than making assumptions. A developer who says, "Can you clarify what 'done' means for this task?" prevents days of rework. A project manager who asks, "What's blocking you right now?" uncovers risks long before they appear in a dashboard. These questions feel casual, but they build a shared mental model that no Gantt chart can replicate.
Another telling habit is the ratio of acknowledgments to corrections. Teams that default to "Yes, and..." rather than "No, but..." tend to surface problems earlier. Consider two responses to a proposed deadline shift. One person says, "That won't work because testing always takes longer." Another says, "I see why you'd suggest that; from past sprints, testing has taken about 20% longer — can we adjust the buffer?" The second version doesn't just disagree; it anchors the disagreement in shared history. Projects with more of this "constructive friction" report fewer surprise failures, even when total talk time stays the same.
Finally, watch how often team members close the loop without being asked. The phrase "I'll take a look and get back to you by Thursday" is common, but the habit that matters is actually following up — even if only to say, "Still investigating, no update yet." Silence creates ambiguity, and ambiguity compounds across distributed teams. One study of software teams found that projects where more than 60% of messages received a reply within one business day completed on time at nearly twice the rate of those with lower response rates. This isn't about constant availability; it's about making implicit commitments visible through ordinary speech.
FAQ
Ask them to walk you through a recent custom design from sketch to tooling. A genuine in-house team will be able to discuss specific challenges—like how they adjusted contact dome geometry to hit your exact force curve—without needing to 'check with the factory.' Look for names, not departments. If every answer routes through a sales rep, the engineering depth probably isn't there.
Depends on the supplier's process control, but a solid partner will commit to ±10% on actuation force and ±0.1mm on travel without flinching. The real test is whether they provide per-batch SPC data instead of just a certificate. If they can't show you how they control dome placement and contact gap during high-speed assembly, those tolerances mean nothing.
You want a DFM report that calls out undercuts, draft angles, and weld line positions for the housing. Also request a full material datasheet for the contact dome—plating thickness, base alloy, temper. If the supplier pushes back on sharing copper alloy specs or electrical lifecycle test data, that's a sign they're sourcing commodity domes and calling them 'custom.'
Ask for their internal reject rate on custom tactile switch lines over the last six months, and then ask what the top three failure modes were. A healthy supplier will name specific issues—like dome collapse after 200k cycles or intermittent contact from flux wicking—and explain the corrective action. Vague answers like 'we have zero defects' are worse than a high reject rate.
Most serious suppliers quote MOQs between 5,000 and 50,000 pieces, driven by reel packaging and assembly line changeover time. If someone offers an MOQ of 500, they're either hand-soldering domes or absorbing cost to win your business—both of which create reliability or pricing surprises later. Ask what happens to unit price at 5k, 20k, and 100k pieces to see the real cost curve.
Before sharing full drawings, ask if they're willing to sign a mutual NDA that covers tooling drawings, dome profiles, and firmware test parameters—not just the final part. Also split the supply chain: have them manufacture housings and domes but assemble elsewhere, or at least request dual-sourcing for critical components. If they refuse to disclose sub-supplier names, walk away.
Beyond lifecycle (at least 200k actuations at your specified force), you need a contact resistance stability test under temperature cycling from -20°C to 70°C, and a solder heat resistance test showing no dome deformation after reflow. Also check for 'chatter'—bouncing signals during actuation—using an oscilloscope at 1kHz sampling. Many suppliers only test at 100Hz and miss short-duration opens.
Standard tooling for a custom tact switch housing and dome takes 4-6 weeks, plus 2 weeks for first samples. If they promise 2 weeks total, they're either modifying an off-the-shelf mold or cutting corners on surface finish. Ask to see their mold flow simulation report—if it's missing, the tooling design hasn't been validated and you'll face endless tweaks after sampling.
Conclusion
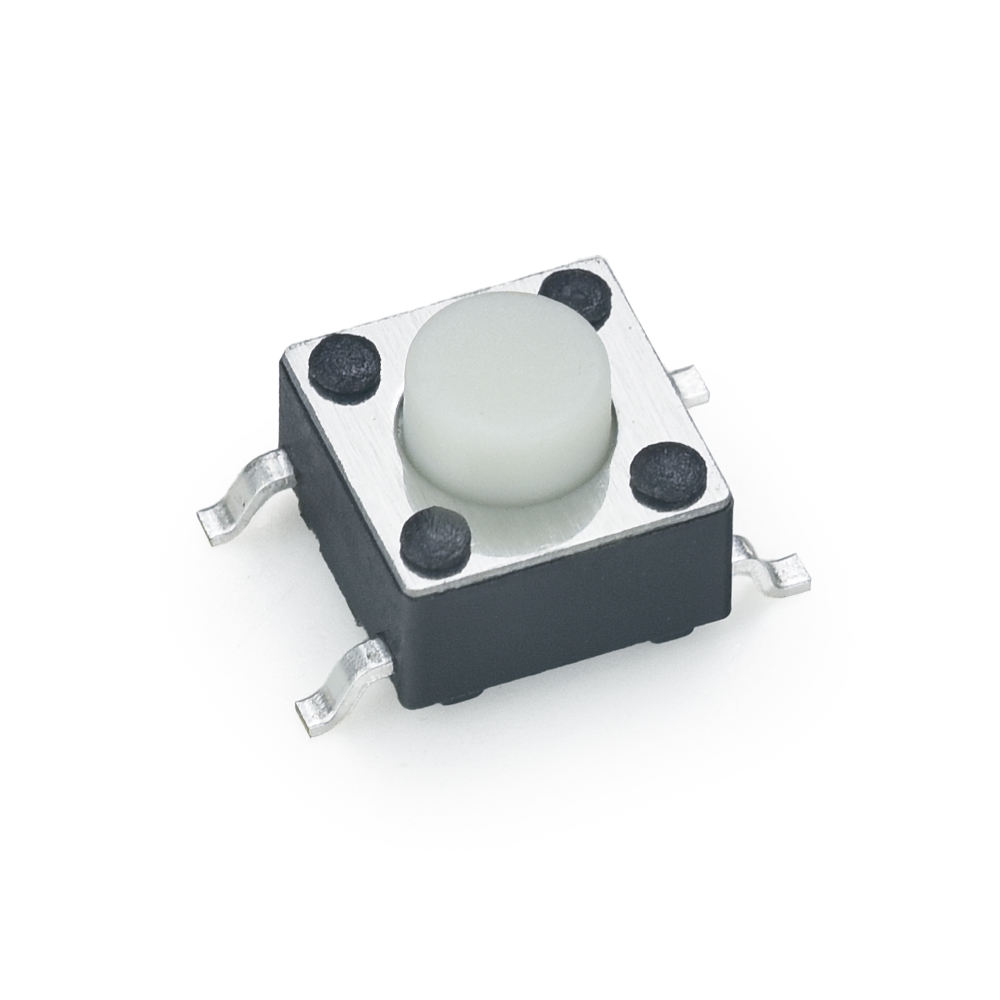
Custom tactile switch programs rarely fail because of the switch itself. More often, the gap shows up in how a supplier handles the step between a drawing and a dependable part. A real engineering partner will question your spec—actuation force, travel, lifespan, plating—not just quote against it. They understand that standard catalog items can’t always absorb your design’s tolerance stack or environmental stress. Ask for material traceability early: not just a certificate, but a willingness to discuss what happens when a specific stainless steel dome or high-temp polymer falls out of stock. That honesty about trade-offs (slightly softer click for better corrosion resistance, for example) is worth more than a perfect initial sample. Also trace how they manage the transition from first article to mass production. Many suppliers can hand you five perfect pieces; the real test is whether their process control holds at 50,000 pieces with the same contact resistance and tactile ratio. If they can’t explain their in-line checks, fixture strategy, or how they handle a dimple height drift, assume you’ll be the one discovering it later.
Quality assurance shouldn’t be a final inspection gate where a worker clicks a button. Look for evidence of process-level thinking: SPC on actuation force, periodic dome lot validation, salt spray or life-cycle testing done on actual production runs, not just pre-production golden samples. Equally important is the supplier’s supplier. If they can’t tell you where their metal domes, base resin, or terminal plating come from—and what happens if that source changes—you inherit that risk without any control. A good custom switch partner will disclose second-tier dependencies and have a documented substitution approval process. Finally, watch communication habits during the quoting and sampling phase. Do they answer the question you asked, or the one they wanted you to ask? Do they flag a tolerance conflict before you find it in testing? Do they share weekly updates without being chased? Those small signals predict how they’ll behave when a production line is down and a shipment is late. A supplier who is proactive, specific, and slightly boring in their follow-up is usually the one who won’t surprise you later.
Contact Us
Contact Person: Anna lin
Email: [email protected]
Tel/WhatsApp: +86 13567768885
Website: https://www.kjele.com/