High Quality Megasonic Cleaning System: How to Choose the Right One
2026-10-04
If you've ever compared megasonic cleaning systems, you know the specs all start to blur—same frequencies, same power ratings, same bold claims. Yet in production, the differences become painfully obvious: one system leaves parts spotless, another leaves a thin film of failure. Choosing the right high-quality megasonic cleaning system isn't about luck; it's about knowing which design details actually drive performance. That's what we focus on at Siansonic. In this guide, we'll cut through the noise and show you exactly what to look for before you buy, so your next cleaning system works as hard as you do.
The Frequency Sweet Spot: Why 40 kHz Isn't Always the Answer
If you've ever shopped for an ultrasonic cleaner, you've probably seen 40 kHz plastered everywhere. It's the default setting for good reason: it handles everyday grime on jewelry, eyeglasses, and small metal parts without much fuss. But treating 40 kHz as a one-size-fits-all solution overlooks how cavitation actually behaves at different frequencies.
Lower frequencies around 25 kHz produce larger, more energetic bubbles that collapse with enough force to knock loose heavy carbon deposits or chunky contaminants from rugged industrial components. That same aggressive cleaning, however, can etch softer surfaces or damage delicate finishes. Higher frequencies, say 80 kHz or 120 kHz, generate smaller bubbles and gentler scrubbing action, which reaches into microscopic crevices and cleans precision parts without surface erosion.
So the sweet spot isn't a fixed number—it's a match between frequency, contaminant type, and material tolerance. A machinist degreasing steel fixtures might get better results at 28 kHz, while a lab cleaning fragile glassware or printed circuit boards will likely prefer 80 kHz or above. The next time someone claims 40 kHz works for everything, remember that cleaning is more like tuning an instrument than flipping a switch.
Matching the Transducer to Your Part Geometry
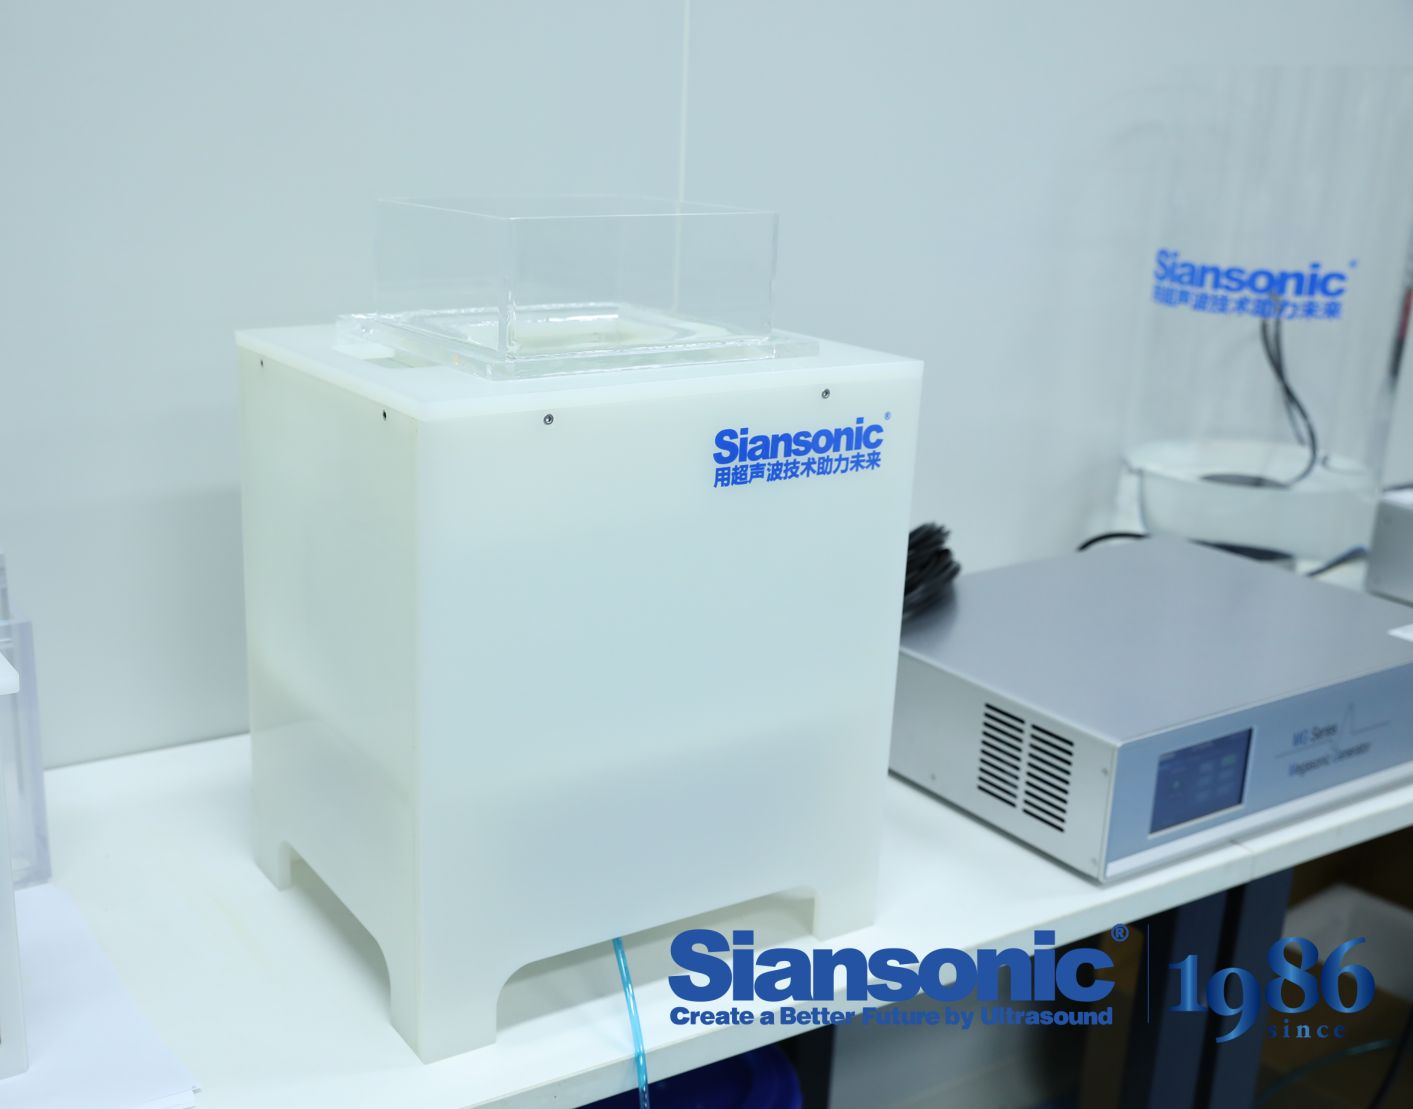
Getting the transducer to sit well against your part isn't about forcing a standard face onto a curved surface. Start by mapping the contact zone with a quick visual inspection or a simple contour gauge. If the part has a slight crown or a fillet, even a small air gap can throw off the reading. Choose a transducer with a replaceable wear face or a flexible delay line that can conform just enough without losing energy. You might also machine a small concave shoe that matches the radius—it takes ten minutes but keeps the signal strong and repeatable.
For parts with tight corners, deep grooves, or threaded ends, a long rigid probe rarely works well. Instead, look at right-angle transducers or those with slim, pencil-style tips. The key is to keep the active element perpendicular to the surface you care about. If the geometry forces an awkward angle, a small wedge or a custom contoured buffer rod can redirect the beam. Test on a scrap piece with a known flaw first; if the echo comes back clean and the baseline stays flat, you've found the setup.
Don't overlook the couplant. On rough or pitted surfaces, a heavy gel can bridge tiny irregularities, but it also adds a slight delay. A thin oil works well on smooth, machined faces. For oddly shaped parts, try a soft membrane couplant or even a water column if you can set it up. The goal is a stable, low-noise signal that doesn't drift as you move along the geometry. If the transducer rocks or loses contact at the edges, go back to the contour—sometimes a slight hand rotation makes all the difference.
Fluid Dynamics and Temperature: The Quiet Performance Killers
Most performance discussions gravitate toward horsepower, clock speeds, or raw material strength, yet the real culprits behind gradual efficiency loss often hide in plain sight. Fluid dynamics and temperature rarely announce themselves with a sudden failure. Instead, they erode output silently—through drag that steals momentum from moving parts, through thermal expansion that tightens clearances, and through viscosity shifts that force pumps and bearings to work harder for the same result.
In any system where air, oil, coolant, or fuel flows, boundary layers and turbulence quietly convert kinetic energy into heat. A poorly shaped intake runner or an overlooked bend in a cooling line can cost more power than a ten percent reduction in mechanical friction. Meanwhile, temperature compounds the problem: as components heat up, seals soften, lubricants thin out, and electronic sensors drift. The performance curve doesn't just dip—it degrades unevenly, making diagnosis tricky because the system still appears functional under casual observation.
What makes these two factors especially insidious is their feedback loop. Higher fluid resistance generates more heat, and that heat further degrades fluid properties and dimensional tolerances. Breaking the cycle demands attention to details that rarely appear on spec sheets: surface roughness inside passages, thermal soak patterns after shutdown, or the way a fan shroud redirects airflow at partial load. Until those quiet killers are addressed, every other upgrade simply fights against a rising tide of invisible losses.
Power Density Without the Damage: Walking the Cavitation Tightrope
Achieving high power density in ultrasonic systems often tempts engineers to push amplitude limits, yet cavitation erosion quietly eats away at transducer faces and reactor walls. The damage shows up as pitting, material loss, and eventual failure, forcing a trade-off that many accept as unavoidable. But what if the real problem isn't the energy itself, but how it's delivered?
Walking the cavitation tightrope means shaping the acoustic field so that collapse events stay in the bulk liquid—not on solid boundaries. Pulse modulation, swept frequencies, and carefully tuned standoff distances can spread the collapse energy across a larger volume. The result: intense sonochemical activity without the localized hotspots that chew through stainless steel or titanium.
Field data from industrial cleaning and wastewater reactors shows that operators can hold power densities above 50 W/cm² for months without measurable erosion, as long as the duty cycle and frequency sweep are optimized. It's not about dialing back the power; it's about respecting the physics of bubble dynamics. The tightrope exists, but it's wider than most people think.
Maintenance Realities: What the Spec Sheet Won't Tell You
Most spec sheets quote service intervals based on clean, climate-controlled test environments. On a real job site or workshop floor, dust, humidity, temperature swings, and irregular duty cycles throw those numbers out the window. You'll end up changing filters, greasing fittings, and checking fasteners twice as often as the manual suggests, especially if you run equipment near abrasive particles or in high-moisture areas.
The real cost of upkeep rarely appears in the purchase price. Proprietary lubricants, specialized diagnostic adapters, software subscription fees for firmware updates, and calibration services can add up fast. Some machines use uncommon bearing sizes or sealed assemblies that force you to replace an entire module instead of a $5 part. Before buying, ask about lead times for wear items and whether local technicians are actually certified to work on the model—not just "authorized" on paper.
Design choices that look great in a brochure often create maintenance headaches. A tight engine bay might make a simple belt adjustment take three hours, while a low-profile housing blocks access to the drain plug. Even routine tasks like checking fluid levels or swapping an air filter can require removing guards, panels, or other components. Plan for downtime realistically: a machine that claims "tool-free maintenance" may still need a breaker bar, a heat gun, and a lot of patience when something seizes or corrodes.
Integration Headaches: Making the System Work With Your Existing Line
Trying to bolt a new system onto a production line that's been running for years is rarely a clean plug-and-play affair. The machines already speak their own dialects, conveyors run at slightly different speeds than the spec sheets claim, and your maintenance crew has a few undocumented workarounds they never wrote down. You'll spend more time mapping sensor outputs and timing handshakes than anyone budgeted for, and that's before you discover the old PLC's scan cycle is just slow enough to cause intermittent missed triggers.
One approach that saves a lot of grief is to treat the integration as a negotiation rather than a retrofit. Instead of forcing the new system to assume total control, give it a defined set of responsibilities and let the existing line keep doing what it already does well. That might mean adding a small buffer zone where the new module can operate at its own pace, or using a simple gateway to translate protocols without rewriting the legacy logic. It's not elegant, but it means you can start seeing value in weeks instead of waiting for a full line overhaul that never gets approved.
The real trick is to test with your own parts, not the vendor's demo units. Run a few hundred of the products that actually cause trouble — the odd-shaped ones, the slightly warped trays, the labels that peel just enough to confuse a sensor. Once you've logged the failure modes on paper, you'll have a concrete list to hand to your integrator instead of a vague sense that "the timing feels off." That list becomes your acceptance criteria, and it's what turns a frustrating integration project into something your operators actually trust.
FAQ
Start with the transducer array. It should deliver uniform acoustic energy across the entire bath, not just the center. Check whether the generator allows fine control over frequency and power, because different particle sizes respond to different energy levels. Material compatibility matters too—some systems work fine with quartz or sapphire but struggle with softer substrates. Also confirm the filtration loop can handle the expected particle load without clogging, and that the tank drains completely between batches.
Lower frequencies in the 40–80 kHz range create stronger cavitation that removes larger debris but can etch delicate surfaces. Higher frequencies around 1 MHz or above produce gentler, more precise scrubbing at the submicron scale. Most high-quality systems let you sweep or adjust the frequency to match the contamination type. If you're cleaning polished optics or semiconductor wafers, lean toward the higher end; for machined metal parts with heavy grease, lower frequencies work faster.
Transducers convert electrical power into acoustic waves, and any inconsistency shows up as dead zones or hot spots in the bath. Cheap transducers drift over time, reducing cleaning efficiency without warning. High-quality units use matched piezoelectric elements with robust bonding, so the acoustic field stays stable for years. Ask the vendor about mean time between failures and whether individual transducers can be replaced without scrapping the whole array.
Megasonic energy amplifies whatever liquid is in the tank, so the chemistry must be chosen for the specific residue and substrate. Sometimes deionized water with a surfactant is enough; other times you need a solvent blend or alkaline cleaner. Avoid chemistries that foam excessively, because bubbles scatter the acoustic waves and ruin uniformity. Run compatibility tests on scrap parts first, especially for plastics or coated surfaces.
Measure the largest part or basket you plan to clean, then add at least 20% clearance on all sides so the acoustic field can develop fully. Consider how parts will be oriented—vertical racks work better for flat wafers, while mesh baskets suit small components. If you're cleaning multiple batches per hour, look for systems with dual tanks or an automated lift so you don't waste time draining and refilling.
Plan on weekly inspections of the filtration system and monthly checks of transducer connections. The tank should have a sloped bottom and large drain port to prevent residue buildup. Some systems include self-diagnostics for power output and liquid level, which saves a lot of guesswork. Replace filters on a schedule based on particle load, not just when they clog. If the vendor offers a preventive maintenance kit, it's usually worth the cost.
Ask for a demo with your actual parts, not just a standard coupon. Measure particle removal with a surface scanner or microscope before and after cleaning. Request acoustic field mapping data from the manufacturer—it should show variation under 10% across the working area. Check for audible noise and mechanical vibration during operation, as excessive either can indicate poor transducer design. Finally, talk to existing users who run similar processes to see how the system holds up after a year of production.
If your cleaning is a batch process with manual loading, a standalone unit is simpler and cheaper. But if you're feeding a continuous production line—like semiconductor wafers moving from CMP to inspection—then an inline system with robotic transfer and process sequencing makes more sense. Look for modular designs that let you add tanks or change chemistry later without replacing the whole line. The key is matching the automation level to your actual throughput, not over-engineering for imagined growth.
Conclusion
Choosing a high-quality megasonic cleaning system rarely comes down to a single spec on a datasheet. The 40 kHz frequency often gets treated as a default, but that assumption breaks down once you map the acoustic energy to the actual part geometry. A transducer that works beautifully on a flat wafer can create uneven cleaning or even damage on a textured surface or a delicate MEMS structure. Pairing the transducer design with the shape and material of what you are cleaning matters more than chasing a higher wattage number. Likewise, the fluid path and temperature control can quietly wreck your results if ignored. Degassing, flow rate, and stable thermal conditions shift how cavitation behaves, and a system that overlooks these will deliver inconsistent output even with a correct frequency.
Power density is another place where the line between effective and destructive is thin. You want enough energy to dislodge submicron particles without eroding fine features, so the ability to adjust power across the tank or nozzle matters. Then there is the reality after installation: filters, transducers, and seals wear out in ways the spec sheet never mentions, and a cheap system can turn into a maintenance sink. Integration into an existing line also deserves early attention, because a system that cannot communicate with your current robotics, PLCs, or data logging will create downtime no cleaning performance can offset. The right choice usually comes from testing on your own parts under realistic fluid and temperature conditions, not from a polished brochure.
Contact Us
Contact Person: Ivy Zhang
Email: [email protected]
Tel/WhatsApp: +86 1081502288
Website: https://www.siansonic.com/