OEM Children School Socks How to Choose the Best Bulk Supplier
2026-10-17
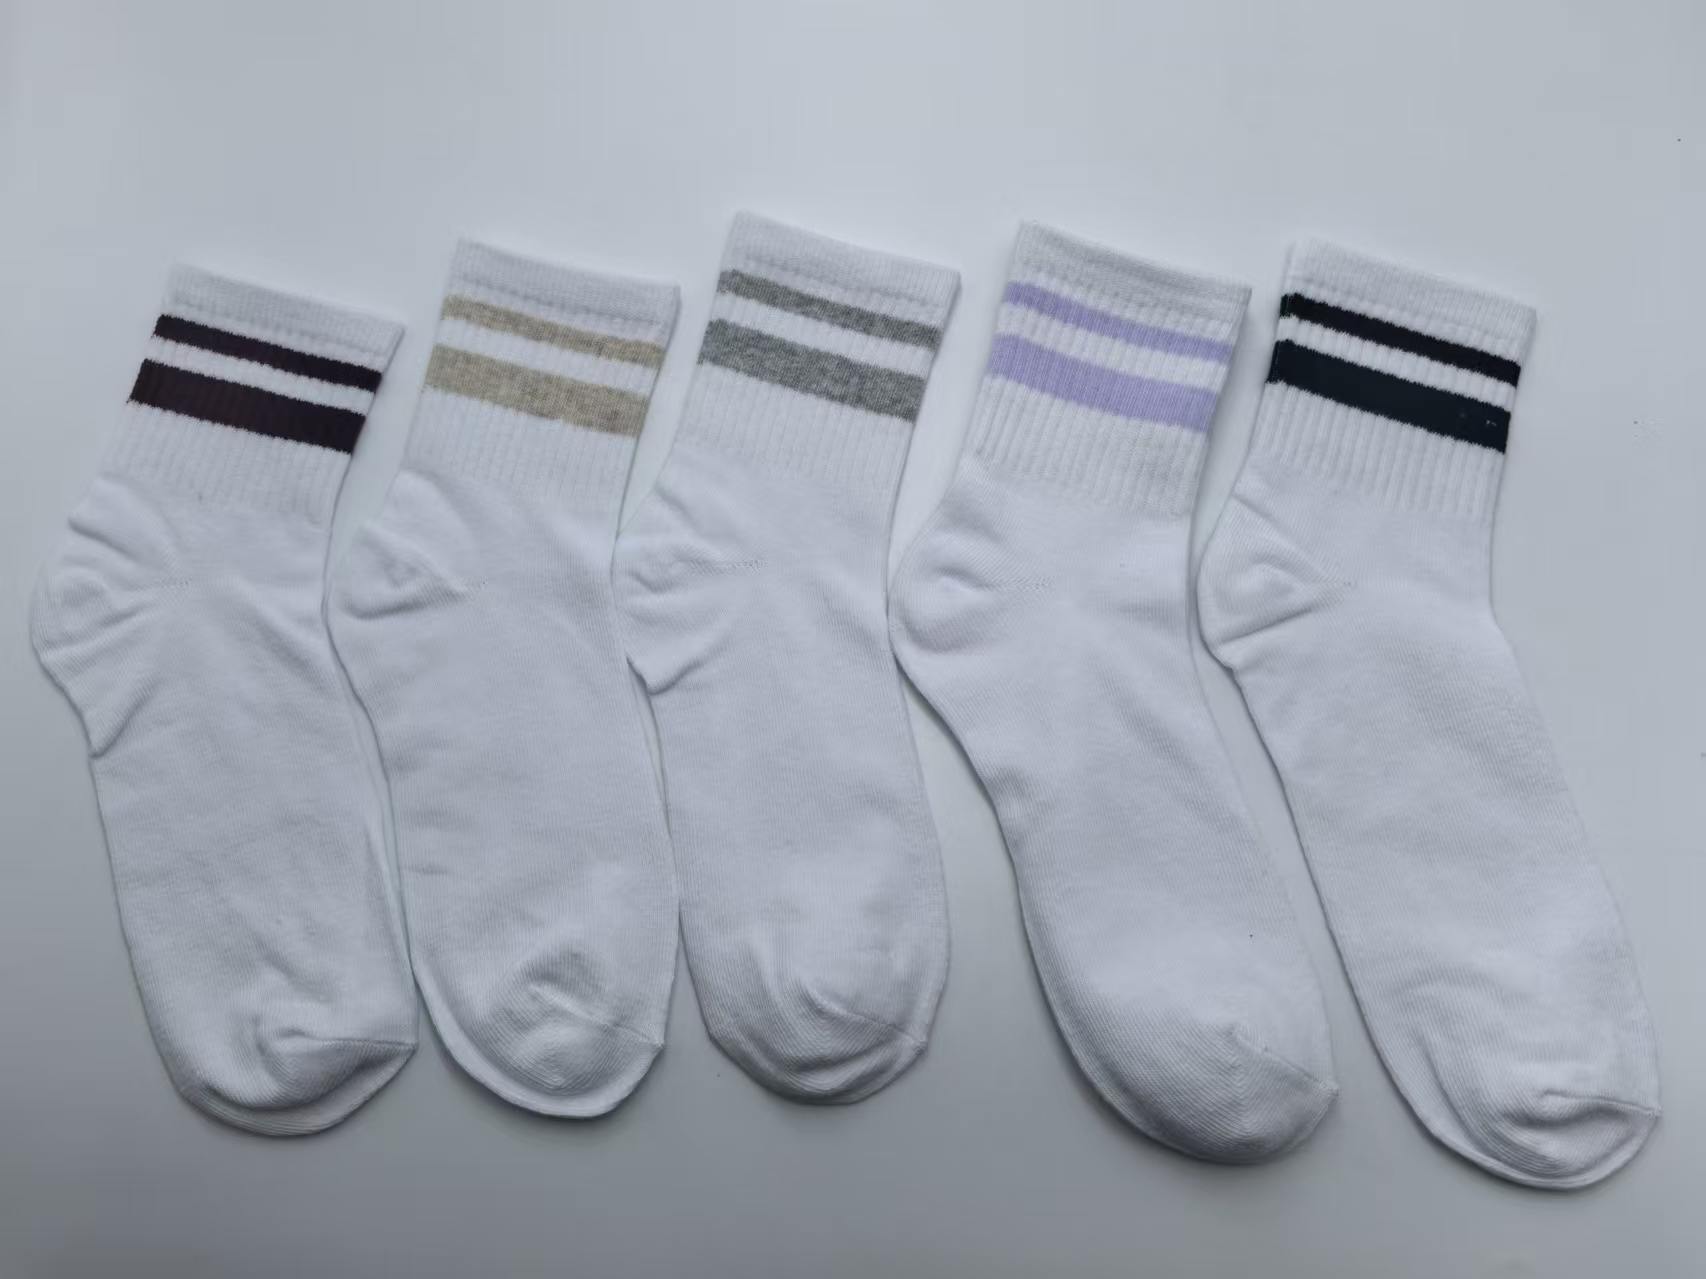
Finding the right OEM children school socks supplier can make or break your retail or wholesale business. From fabric durability to elastic comfort, a single misstep leaves parents complaining and kids tugging at their ankles. The bulk market is crowded, and many suppliers promise quality they never deliver. So how do you separate dependable partners from costly mistakes? This guide walks you through exactly what to check—from material blends and sizing consistency to ethical production and packaging—before you place your first large order. And if you're looking for a name that consistently passes these tests, KINDWAY has built a reputation around school socks that survive playgrounds, washes, and growing feet. Read on to avoid the most common sourcing traps and choose a supplier that keeps customers coming back.
Material Choices That Survive Playgrounds and Washing Machines
A playground is basically a full-body abrasion test: slides, rubber mats, wood chips, and the occasional face-first tumble all grind away at fabric. If you pick a lightweight single-knit cotton, expect it to pill, thin at the knees, and develop holes by mid-summer. The right material choice starts with a tight, heavy weave that can take friction without shredding.
Heavy cotton twill, denim-weight canvas, and nylon-blend ripstop hold up far better than soft jersey knits. Look for double-layer knees and reinforced seat panels instead of relying on a single layer of fabric. Color also matters: pigment-dyed or yarn-dyed colors won’t fade into a sad, washed-out version of themselves after ten trips through the machine.
Then there's the washing machine itself. Hot water, enzyme detergents, and a hot dryer cycle can break down weak fibers faster than any playground. Fabrics with tightly twisted yarns and high abrasion resistance survive this routine without losing shape. Avoid anything labeled 'hand wash' or 'lay flat to dry' unless you enjoy adding another chore to an already long list.
Reading Between the Lines of Factory Audit Reports
A clean scorecard rarely tells the whole story. Experienced sourcing managers learn to look past the final grade and study the language of individual findings. Phrases like "minor discrepancies were noted" or "the facility has demonstrated a commitment to improvement" often signal deeper, unresolved issues that the auditor chose to soften. Compare the number of observations against the severity ratings: a report with fifteen low-risk findings may actually reflect a systemic problem in documentation, while a single critical finding buried near the end can reveal a safety hazard that the summary conveniently downplays.
The real value lies in what is not explicitly stated. Audit reports are snapshots taken on a particular day, under a specific set of conditions. Notes about worker interviews being conducted "away from management presence" or "records were made available upon request" can suggest that access was controlled or that responses were rehearsed. Pay attention to the auditor's choice of verbs. "Verified" implies direct evidence, while "was informed" or "according to management" indicates secondhand assurance. These linguistic shifts separate a genuinely transparent factory from one that has learned to perform compliance.
Lastly, compare trends across multiple audits. A single report may show a passing score, but a series of reports from the same facility often reveals patterns that a standalone review misses. For example, if the same minor issue appears in three consecutive audits, it is not minor at all; it is a sign that corrective actions are superficial. Likewise, sudden improvements in one area after years of stagnation may indicate that the factory has hired a consultant to polish the paperwork rather than fix the root cause. Reading between the lines means treating each report as one chapter in a longer narrative, not as the final word.
Sampling Tricks to Spot Color Bleed and Elastic Failure Early
Most print shops catch color bleed when it's already ruined a run. A smarter move is to pull samples at the exact moment the press hits steady-state temperature, not after a few hundred sheets. Run a small batch of the most saturated ink combinations -- heavy magenta next to a pale yellow, for instance -- and immediately check the back side under oblique light. If you see a faint halo before the stock cools, you've got a bleed risk that only gets worse with humidity.
Elastic failure hides in the stretch, not the snap. Cut narrow strips from the edge and center of the sheet, then fold them sharply along the grain and against it. Don't just look for cracks; run a thumbnail along the fold line while pulling gently. A good stock will spring back with barely a mark. If the surface develops a whitish line or the fibers separate on the third pass, that's the early warning -- the kind you'd normally miss until a die-cut job tears on the folder.
Pair the two tests on the same sample whenever possible. A sheet that passes the bleed check but starts to delaminate under repeated flexing points to a coating problem, not a paper defect. Keep a small log of which batches show micro-cracking at low fold counts. After three runs you'll know exactly which supplier's stock is lying about its elastic range, and you'll catch it before the job hits the bindery.
Custom Tags, Polybags, and Small Details Parents Notice
Parents often spot things before kids do—a scratchy tag poking out from a collar, a polybag with a sharp corner left on the floor, or a tiny stitch that's already fraying. It's these small, almost invisible details that shape how a product feels in daily use. A custom woven label with soft, rounded edges can turn an itchy afterthought into a comfortable touchpoint. Replacing flimsy polybags with resealable, thicker-gauge options makes unpacking less frustrating and keeps small parts contained until playtime begins.
What gets noticed isn't always the headline feature. A snapped button, a dangling thread, or a mismatched snap on a onesie can undo hours of thoughtful design. Parents run their fingers along seams and check how a zipper pull sits against a child's chin. Choosing flat-lock stitching, hidden snaps, and tagless printing shows an understanding of real-world use—no one wants to discover a rough edge at bedtime.
The difference between a product that gets recommended and one that gets returned often lives in these minor choices. A polybag that opens without scissors, a tag that doesn't need cutting out, a hanging loop that actually holds—each small decision adds up. When these basics are handled with care, parents don't mention them in reviews; they simply reorder and tell a friend.
Realistic MOQs and Timelines for Seasonal School Demand
Seasonal school demand rarely behaves like standard retail. A school orders uniforms in June for August, not because that's ideal, but because budgets and enrollments only firm up after spring. Suppliers who quote a 2,000-piece MOQ for a primary school of 400 students are ignoring how PTA committees actually approve purchases. Realistic MOQs for school-specific items—embroidered blazers, house-colored polo shirts, monogrammed backpacks—often start at 300 to 500 units per size run, with some manufacturers willing to split production across multiple schools in the same district to reach viable volumes. This shared-batch approach lets smaller institutions access custom work without warehousing dead stock before the next enrollment cycle.
Timelines need to work backwards from the first day of term, not forwards from purchase order acceptance. A typical custom uniform run requires four weeks for fabric dyeing and cutting, two weeks for embroidery or screen printing, one week for quality control and packing, and another week for shipping and customs if goods cross borders. That's eight weeks minimum without any buffer. Yet many schools issue purchase orders in July expecting delivery by mid-August. Suppliers who have done this before build in a two-week contingency for rework on high-error items like jacket zippers or crest alignment, and they communicate a "no changes after" date for design files. This kind of transparency prevents the last-minute panic that usually lands as emergency air freight charges.
The smartest approach for both schools and suppliers is to treat seasonal demand as a repeated annual event, not a one-off project. Vendors can offer lower MOQs if the school commits to a three-year contract with predictable reorder windows, allowing the factory to reserve capacity during off-peak months. Schools benefit from locked-in pricing and guaranteed delivery slots, while suppliers get smoother production flow and fewer rush orders. In practice, this often means the first year's order carries a slightly higher per-unit cost to cover pattern making and initial setup, with costs dropping in years two and three as the template is reused. Clear communication about these trade-offs—rather than unrealistic promises—keeps the relationship functional through multiple school cycles.
Locking Quality with Reorder Clauses and Defect Penalties
A supplier that ships a bad batch usually hears about it once, maybe twice, before the relationship quietly cools. That changes when the contract ties future reorders directly to defect data. Instead of vague promises of improvement, the reorder clause says: if your defect rate crosses an agreed threshold, the next purchase order shrinks or shifts to an approved alternate. This makes quality tangible on the buyer's side and gives the supplier a reason to track rejects in real time.
Defect penalties do the heavy lifting that inspection alone cannot. A well-written penalty isn't just a fine; it covers sorting labor, line stoppages, customer returns, and the true cost of rework. But the real leverage comes from how penalties interact with reorder clauses. A supplier can absorb a one-time charge, but losing volume on the next three orders changes behavior. That combination locks in quality because the consequences scale with the supplier's own performance, not the buyer's enforcement budget.
There is a difference between a punitive contract and a self-correcting one. The goal is not to punish every defect, but to make poor quality expensive in the places suppliers actually care about: revenue and repeat business. When reorder clauses and defect penalties are calibrated together, the buyer gets a built-in escalation path that works even without constant confrontation. Quality stops being a negotiation point and becomes an operating condition.
FAQ
Look beyond basic certificates. Ask how they handle fiber blending, whether knitting machines are cleaned between color runs, and if the dyehouse tests for restricted substances regularly. Request photos of the same-day production line, not marketing shots. A supplier that can walk you through their reject rate by batch is far more useful than one that only shares a price list.
Ask for wash-test reports from a third-party lab, not just the factory's word. Check if they pre-shrink the yarn or use heat-setting after knitting. Request a sample pair, wash it five times at home, and measure against a new pair. If the supplier hesitates to send a second sample for your own testing, treat that as a warning sign.
MOQs vary widely depending on yarn type and design complexity. For basic solid-color school socks, a supplier might quote 500-1,000 pairs per size per color. For custom stripes or logo knits, expect 2,000+ per design. Always ask whether the MOQ applies per size, per color, or per total order—that distinction changes your cash flow dramatically.
Request current test certificates for OEKO-TEX Standard 100 or similar, and check the issue date—don't accept one from three years ago. Ask which specific yarn supplier they use and whether they can provide batch-level testing for azo dyes, formaldehyde, and heavy metals. A trustworthy factory will name its yarn mill without hesitation.
Never skip the pre-production sample. Pay for two rounds: one factory sample and one gold-seal sample you approve. Keep the approved pair and take photos from all sides. When the bulk arrives, compare randomly selected pairs against that reference. If the supplier wants to charge a sample fee, that's normal—just confirm it's refundable against your order.
Ask about labeling, individual polybagging, inner boxes, export cartons, and loading charges. Some suppliers quote only the sock price and later add 15-20% for packaging and handling. Get the full cost broken down per unit, including any charges for custom inserts or barcode stickers. Also clarify if the freight quote includes customs clearance on their end.
Ask for a real production timeline, not 'usually 30 days.' Find out how many lines they run and which months are peak for school uniform orders. Request a buffer of at least 10 days for dyeing delays or machine breakdowns. A supplier that gives you a single date without mentioning holidays or raw-material lead times is guessing, not planning.
Packaging can be a quiet differentiator. Ask if they can pre-pack by size in sets of three or five, add a simple size sticker, or use recyclable paper bands instead of plastic. The right packaging saves school staff hours of sorting. Make sure any child-safe packaging rules in your market are met, such as no small loose parts.
Conclusion
Choosing a reliable OEM supplier for children's school socks starts with material reality, not just spec sheets. Cotton-rich blends with reinforced toes and heels hold up to playground wear and repeated hot washes, but polyester or nylon content should be limited so feet can breathe. Don't stop at fiber percentages—ask for factory audit reports and actually read the small print. A high score means little if the audit is dated, the production line was idle, or worker turnover is hidden in footnotes. Request pre-production samples and stress-test them yourself: rub a wet white cloth on dark colors to catch dye bleed, stretch the cuffs twenty times to see if elastic snaps back, and run them through a home wash cycle. Details parents notice include soft flat-seam toes, size labels that don't itch, and polybags that can be recycled or clearly state material codes. These small touches signal a supplier that understands school families, not just bulk buyers.
Realistic minimum order quantities and lead times matter as much as fabric quality. Schools order in waves—before autumn and after winter break—so lock your production slot early, but don't accept a MOQ that forces you to overstock unpopular sizes. A good OEM partner will split shipments by size ratio or offer mixed-color runs without insane premiums. Put reorder clauses and defect penalties into the contract before the first container leaves the factory. Specify an acceptable defect rate, usually under 2%, and agree on compensation for late delivery or color mismatches. Also require third-party inspection reports for each batch, not just a final sample. The best bulk supplier is not the cheapest quote but the one whose audit record, sample behavior, and contract terms all point to consistency when your school season hits its peak.
Contact Us
Contact Person: Alfred Lee
Email: [email protected]
Tel/WhatsApp: +86 13806701496
Website: https://www.hainingsocks.com/