Tissue Converting Line Supplier: Essential Questions to Ask Before Buying
2026-10-12
Before you sign off on a tissue converting line, the supplier you choose will shape your production floor for the next decade. That's why the questions you ask now matter more than the quote they put in front of you. Too many buyers focus on speed and price, only to discover after installation that changeover times, support response, or spare parts delivery don't match the sales pitch. This guide breaks down the essential questions to put to any tissue converting line supplier—so you can avoid those expensive surprises. If you've ever wondered what separates a vendor from a true partner, DAXIN sets a good benchmark for transparency. Here's what to ask before you commit.
How Much Real-World Output Can You Expect After the First Month?
Most people finish their first month with a handful of rough drafts, a clearer sense of what actually eats up their time, and maybe one or two small wins that feel almost accidental. You won't have a polished portfolio, a steady stream of customers, or a finished manuscript. What you will have is data: which hours you actually sat down to work, which tasks you kept avoiding, and whether your initial plan matched how you operate day to day.
A fair expectation is somewhere between three and ten concrete outputs, depending on the field. A writer might complete two short pieces and outline a longer one. A developer might ship a small utility or fix a batch of bugs on an existing project. A freelancer might land a single low-paying gig that came from a warm referral rather than cold outreach. The common thread isn't volume, it's that you now have artifacts you can point to, even if they're rough around the edges.
If you find yourself with nothing to show after thirty days, the problem is rarely talent. It's usually that the goal was too vague or the schedule was built around motivation instead of a fixed block of time. Treat the first month as a diagnostic period: lower the stakes, narrow the scope to one repeatable action, and let the output be ugly. That's the only way the second month has a chance to produce work you're actually proud of.
Which Roll Formats, Ply Counts, and Fold Types Are Actually Feasible?
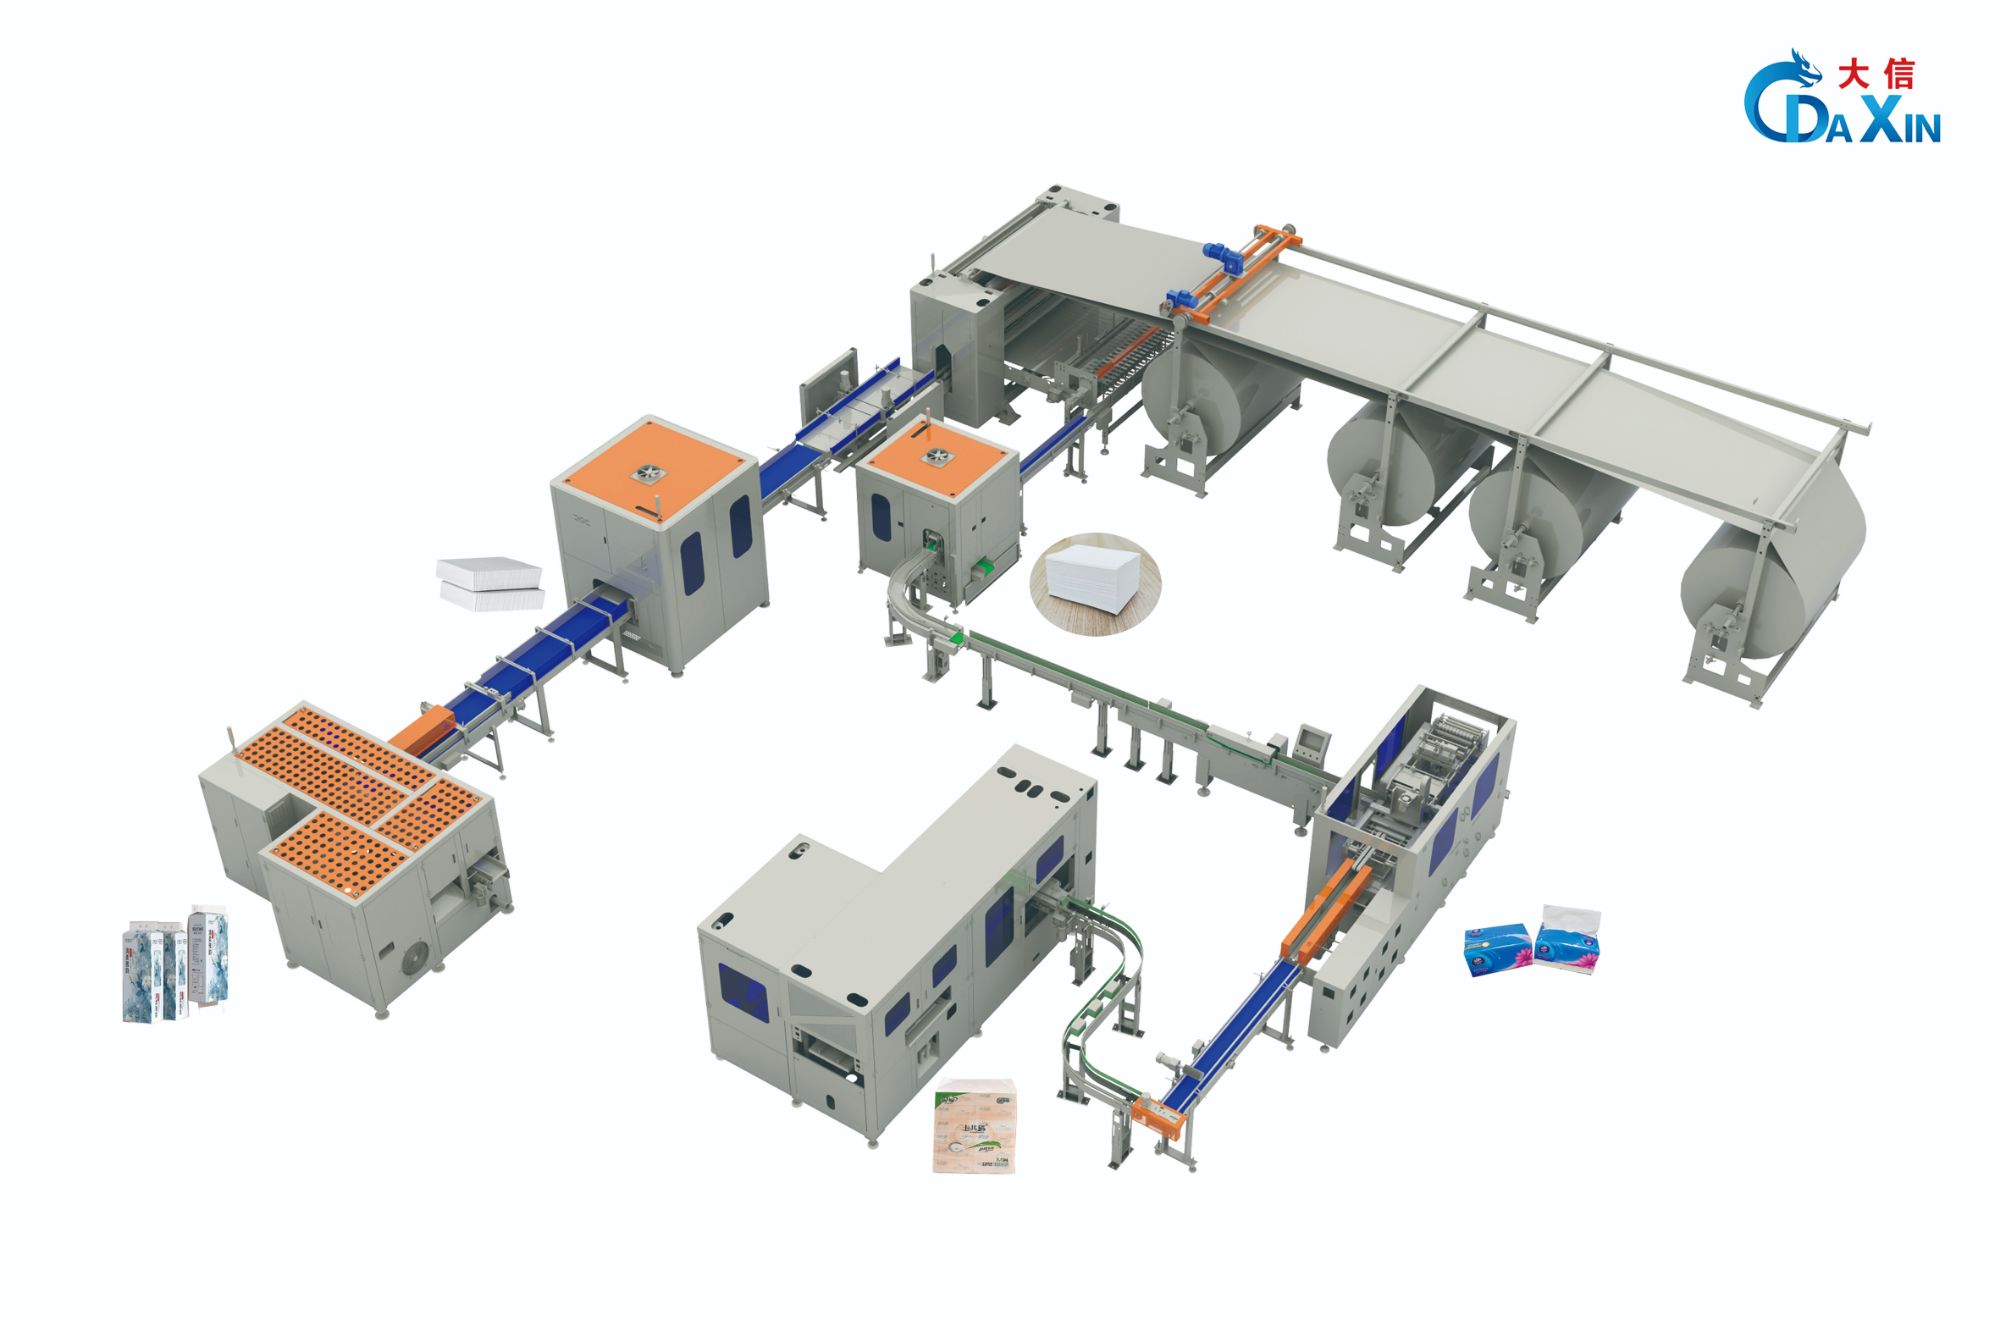
When you move beyond what appears on retail shelves, the range of roll formats that can actually be produced is narrower than most buyers assume. Roll diameter, core size, sheet length, and perforation spacing all interact with the winding equipment and downstream converting lines. For instance, a 4.5-inch diameter roll with a 1.5-inch core is straightforward on most high-speed winders, but pushing beyond a 9-inch diameter often requires slower cycle times or custom mandrels, which makes the format less practical for high-volume runs.
Ply count follows similar logic. Two-ply is the default for most away-from-home and retail tissue because it balances bulk, softness, and runnability. Single-ply remains workable for high-traffic settings where cost per sheet matters more than hand feel, while three-ply and four-ply products are feasible only on lines designed with enough embossing and lamination stations. Beyond four plies, converting speeds drop sharply and the risk of ply separation during winding rises, so those constructions are usually reserved for niche or premium short runs.
Fold types add another layer of constraint. C-fold and multifold towels dominate because they can be produced on continuous-feed folders at high output, but interfolded configurations demand precise sheet registration and often dedicated stacking equipment. Quarter-fold and dispenser-fold napkins are feasible when the parent roll width and cut-off length are matched to the folder geometry, yet uncommon fold patterns can force frequent changeovers, lower throughput, and higher waste. In practice, the most feasible combinations are those a converter already runs routinely; anything outside that window may be technically possible but rarely economical.
What Happens When a Critical Component Fails on a Weekend Shift?
A Friday night handoff leaves a skeleton crew. At 2 a.m. Saturday, a bearing seizes on the main conveyor motor. No spare in the crib. The on-call supervisor wakes a distributor rep, but the part is three states away. Production halts.
Weekend shifts often lack the specialized technicians who know the machine's quirks. The junior operator tries a workaround—bypassing a sensor—but risk management shuts that down. Meanwhile, orders pile up.
By Monday morning, the failure has cost more than the component. Overtime, expedited shipping, and missed delivery windows stack up. A debrief reveals that the critical spare was flagged for restock two weeks earlier but never ordered.
Can Their Automation Level Work With the Operators You Already Have?
A lot of automation pitches assume you'll replace your team or retrain everyone from scratch. That's rarely practical. The real question is whether the system's interface and daily operating logic line up with what your current operators already understand. If the automation expects someone with an engineering background to babysit it, but your floor staff are experienced machine operators who rely on visual checks and manual overrides, you'll hit friction almost immediately.
Look closely at how the automation handles exceptions. Some systems are designed to run unattended until something goes wrong, then require a specialist to diagnose. Others are built around operator prompts—clear, simple instructions that a skilled but non-technical person can act on. Ask the vendor to walk through a realistic failure scenario with your own team. If your operators can't follow the response steps without extra notes, the automation level is probably too detached from their current workflow.
Training matters, but it shouldn't be a complete reset. The best fit is when the automation amplifies what your operators already do well—reducing repetitive setup, flagging issues earlier, or handling fine adjustments—without demanding they learn a new programming language or abstract control theory. If you have to build a parallel support team just to keep the automation running, the level is wrong for your operation.
Will They Connect You With Tissue Mills Running Similar Products?
Finding a supplier who already works with mills producing comparable tissue grades can save you months of trial runs. Ask directly whether they have active relationships with facilities that run similar furnish mixes, basis weights, and converting lines. A yes should come with specifics—machine widths, daily output, and typical end-use applications—not vague assurances.
Beyond a simple introduction, clarify what “connect” actually means here. Some brokers will only pass along a mill name and let you handle the rest, while others stay involved through sampling, trial coordination, and first production runs. The difference shows up quickly in how smoothly your spec gets translated on the floor.
If they hesitate or dodge the question, treat that as a red flag. Strong networks in tissue aren’t built overnight, and a partner who can’t name at least two mills running products like yours probably lacks the depth you need when demand shifts or quality issues arise.
What Are the Honest Utility Consumption Numbers for Your Local Costs?
When your last power bill landed, did the kilowatt-hour figure actually match what you expected? Most people scan the total, wince, and move on. But the honest consumption numbers hide in the usage detail: base load from fridges and always-on electronics, seasonal spikes from cooling or heating, and the phantom draw you forgot about. Pull twelve months of statements, not just last month, and average the kWh or therms. That's the real starting point before you compare rates or blame the utility.
Local costs vary more than most realize, sometimes by twenty or thirty percent within the same postal code. Your neighbor's "cheap" bill might reflect a different rate plan, a newer water heater, or a home that faces north. So don't copy their setup — calculate cost per unit from your own data. Divide total bill by consumption, then watch how fixed delivery charges ride on top. If solar or time-of-use pricing is involved, pull the hourly breakdown from your meter. The honest number is never the advertised rate; it's what you actually paid per kWh, therm, or gallon over time.
Once you know your true baseline, small changes stop being guesswork. Replacing a twenty-year-old freezer may save eight dollars a month, or it may save two. Insulating an attic shows up not in the salesman's estimate but in the December versus June gap. Track consumption before and after any upgrade with the same billing cycle, not the same calendar month. Utility data is messy, but it's the only honest yardstick for local costs.
FAQ
Our line handles toilet paper, kitchen towels, and facial tissue from 2-ply to 4-ply, with finished roll diameters between 90 and 150 mm. Changeover between log saw patterns and embossing designs takes about 20 minutes, and we can run both jumbo rolls and pre-cut parent rolls without major modifications.
We send two engineers for on-site installation and commissioning, usually taking three to four weeks. After that, we do five days of hands-on operator training, plus two days for maintenance staff. You also get remote video support for the first three months, which helps with small adjustments and troubleshooting.
A standard line ships in 14 to 16 weeks from order confirmation. Custom features like automatic core feeding or special unwind stands can add three to four weeks. The biggest delay risk is late approval of layout drawings, so we try to lock those down within the first two weeks.
Yes, we have three customers in your region running 4 to 6 tons per day on similar grades. Two of them produce private label toilet paper, and one makes folded kitchen towels. We can arrange a video call or plant visit after signing a basic non-disclosure agreement.
We keep a local stock of wear parts like blades, belts, and embossing rollers for the first year. Emergency orders placed before 2 PM ship the same day by air. For technical issues, our engineers respond within 4 hours by phone or video, and on-site visits are available within 48 hours in most cases.
The standard line includes automatic tension control, web break detection, and a servo-driven log saw. Start-up waste is typically below 1.5% of input, and steady-state waste runs around 0.8% for toilet paper. You can add camera-based defect rejection, which adds about 8% to the total price but cuts waste further.
You'll need a reinforced concrete pad about 200 mm thick, plus compressed air at 6 bar and a 160 kVA power supply. Software licenses for recipe management are included for the first two years, then it's about 1,200 USD per year. We also recommend budgeting 5% of the machine price for spare parts stock.
We run a 72-hour continuous production test at your plant using your own parent rolls. The line must meet agreed output speed, log diameter accuracy, and waste limits. If it fails, we fix it at our cost and repeat the test. Final payment is only due after you sign the acceptance certificate.
Conclusion
Before committing to a tissue converting line, you need to press the supplier on what actually happens after startup. Most vendors quote theoretical speeds, but ask for a realistic number for your first month of running—will you hit 80% efficiency or struggle at 50%? Roll formats, ply counts, and fold types matter just as much. A line that handles 2-ply kitchen towels might choke on 3-ply bath tissue or interfolded napkins. Get the supplier to confirm precisely which combinations their equipment can run without constant changeover pain. And don't skip the ugly scenario. If a critical component like an embosser or log saw fails on a Saturday night, what is the actual response time? A weekend breakdown can idle your whole plant if spare parts sit in another country.
Automation sounds great until you realize your operators have never touched a servo-driven unwind. Ask whether the supplier's controls match the skill level of the people you already employ—training videos are not the same as hands-on commissioning. Also push them to connect you with at least two tissue mills running similar products, not cherry-picked showcase plants. You want to hear from a converter dealing with the same basis weight, embossing depth, and packaging lines. Finally, demand honest utility consumption numbers based on your local electricity, gas, and water rates. A line that saves 10% on labor but doubles compressed air use might be a terrible deal. If the supplier cannot provide these details with a straight face, walk away.
Contact Us
Contact Person: Sam Xie
Email: [email protected]
Tel/WhatsApp: 86-18938538530
Website: https://www.daxin321.com/